
STL · 3MF · MD · PDF
SP Calibration Set: 19 FDM and 4 Resin Calibration Prints with a Measuring and Tuning Guide (Free)
A free, CAD-checked calibration kit: 19 FDM and 4 resin prints, each with a guide to what to measure, what good looks like and what to change.
- Instant download after checkout
- 3 downloads over 30 days, links by email
- Digital files: all sales final. Licenses
About this design
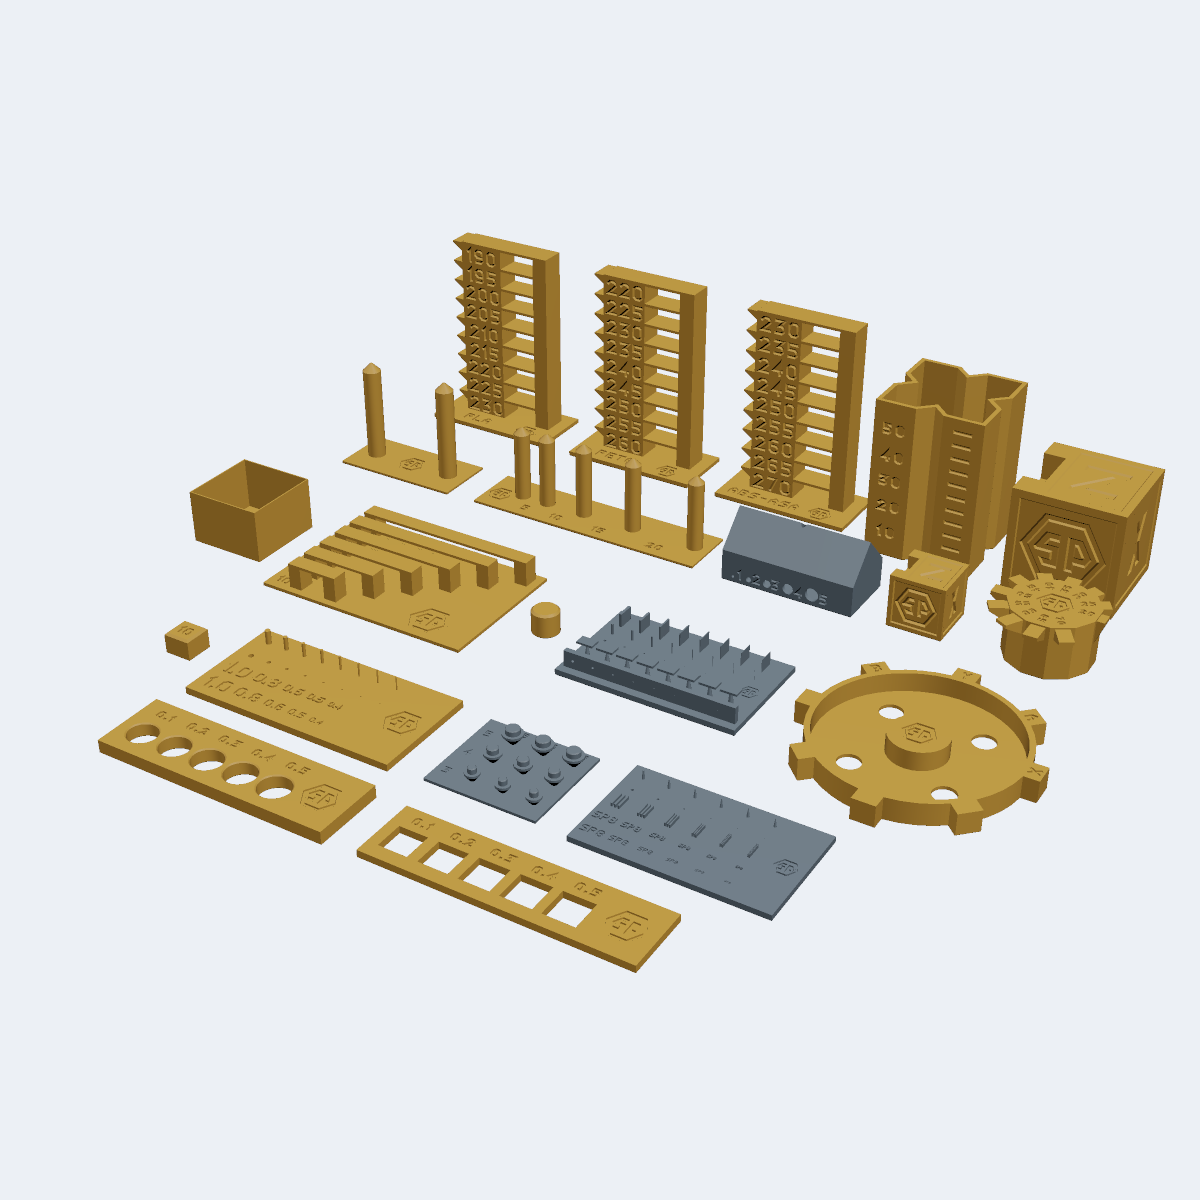
A free, original calibration kit for FDM and resin printers: 19 FDM prints and 4 resin prints, each with a guide to what to measure, what a good result looks like and which setting to change. Every piece carries a small SP hexagon monogram.
Every part is CAD-checked: a closed, watertight mesh whose key dimensions were measured on the exported file. No part needs supports. On the FDM pieces, the only overhangs steeper than 45 degrees are the ones being measured (overhang fan, bridges, temperature tower overhangs and bridges). The resin pieces print straight on the build plate, and an island check found no floating islands on any of them.
The numbers in the guide are typical targets plus CAD and slicer values, not results from printing this kit, so treat them as starting points for your own printer.
Suggested order: print the flow cube and the first-layer test first, then the calibration cube, then the rest in any order. Most people only need the temperature tower for their own material.
FDM pieces (PLA unless noted, 0.2mm layers)
- Calibration cube, 20mm solid: X, Y and Z faces engraved, a stepped notch (10.00mm wide, step at 15.00mm) and the SP monogram for fine detail. Measure on the raised frame rims and aim for within 0.10mm. 3.7g, about 21 min.
- Calibration cube, 40mm hollow: the same layout at double size. Compare it with the 20mm cube to tell a scale error (steps/mm, shrinkage) from an offset error (flow, bulging walls). 22.3g, about 2h 15m.
- Overhang fan: 11 blades with undersides from 20 to 70 degrees in 5 degree steps. The steepest clean blade gives your support threshold angle. 7.0g, about 41 min.
- Bridging test: bridges of 10, 20, 30, 40, 50 and 60mm, decks at 10.00mm. Measure the sag at mid-span and tune bridge fan, flow and speed. 14.8g, about 2h 15m.
- Stringing twin tower: two 7mm towers with a 27mm gap and cone tips. A quick print for retraction changes. 5.3g, about 54 min.
- Stringing 5-pillar: gaps of 5, 10, 15 and 20mm, so you can see how stringing grows with travel distance. 8.1g, about 1h 24m.
- Temperature towers for PLA (230 to 190C), PETG (260 to 220C) and ABS/ASA (270 to 230C): 9 levels in 5C steps, hottest at the bottom. Each level has its temperature engraved, a 55 degree overhang and a 15mm bridge. You add the temperature changes in your slicer; the guide has the height table and a ready-made custom G-code line. 14.9 to 18.2g, about 2h 11m each.
- Tolerance set: a peg plate (round holes) and a fit card (square slots), both at 0.1, 0.2, 0.3, 0.4 and 0.5mm clearance, plus a 10.00mm peg and a 10.00mm key. Find your press fit and sliding fit clearances. 13.3g for all four.
- First-layer plates for 220mm and 256mm beds: five 30 x 30mm single-layer pads (numbered corners, monogram in the centre) inside an outline. Check the pad thickness (0.20mm) and adjust Z offset or levelling per corner. About 1.4g, 9 min.
- Flow single-wall cube: 30 x 30 x 20mm with 0.45mm walls. Measure the wall at 8 points; new extrusion multiplier = old x 0.45 / measured average. 1.9g, about 15 min.
- Pressure / linear advance tower: 40mm square, 60mm tall, V-notches on every side and height marks every 5mm. Ramp the value with height (set-up lines for the common firmwares are in the guide) and read off the sharpest corners: value = start + factor x height. 21.3g, about 1h 51m.
- Small-feature test: pins and blind holes from 2.0 down to 0.4mm, plus raised and engraved text from 1.0 down to 0.4mm stroke. Gives you your design minimums. 8.9g, about 1h 7m.
- Roundness and belt ring: a 70mm ring with eight tabs 80.00mm apart across X, Y and both diagonals. Unequal diagonals point to an out-of-square frame or uneven belt tension. 13.4g, about 1h 36m.
One of each FDM piece: about 174g of filament and 21h 12m of printing (slicer estimates with a generic profile; a tuned printer profile is usually faster).
Resin pieces (0.05mm layers, your resin's normal exposure)
- Exposure matrix: tapered pins (tips 0.5 to 0.1mm), pits (1.0 to 0.2mm), rib gratings (0.6 to 0.15mm) and raised and engraved text. Print it at your current exposure and at plus and minus 15%, then pick the setting where positive and negative features balance. 6.61ml.
- Minimum features and support tips: thin walls, pins, blind holes and sideways holes from 1.0 to 0.1mm, plus eight tabs each held only by one support cone with a 0.15 to 0.8mm tip. Shows the smallest support tip that holds on your printer. 7.97ml.
- Hollow drain shell: 1.6mm walls, drain holes of 1, 2, 3, 4 and 5mm and a 2mm vent. Shows which hole size drains reliably. 6.95ml.
- Drain plugs: nine plugs for the 3, 4 and 5mm holes at 0.05, 0.10 and 0.15mm clearance, on a snap-off sprue. 2.87ml.
All resin pieces: about 24.4ml of resin (model volume; add about 10% for waste and any raft). Wash and post-cure everything the same way before measuring, since curing changes size.
What's included
- Three downloads, so you can pick the one you need: SP_Calibration_Set_Full.zip (all 23 parts), SP_Calibration_Set_FDM.zip (the 19 FDM parts) and SP_Calibration_Set_Resin.zip (the 4 resin parts)
- STL and 3MF for every part, already in print orientation (bottom face down)
- The measuring and tuning guide for every test (GUIDE.pdf and GUIDE.md) and a parts list with key dimensions, grams and print times (info.md), inside each zip
- The guide and each STL and 3MF are also available here as separate downloads.
Print notes
- One FDM set (one of each of the 19 FDM parts): about 174g of PLA and 21h of printing (slicer estimates, generic profile) - Resin parts: 24.4ml in total (model volume; add about 10% for waste) - All parts print without supports - FDM: 0.4mm nozzle, 0.2mm layers, 2 walls, 5 top / 4 bottom layers, 15% gyroid infill, no brim (add a 3mm brim to the small tolerance peg if your bed is slippery) - Print each part as it comes, bottom face on the bed. Use your normal material temperatures except on the temperature towers. - Temperature towers: add the temperature changes in your slicer at the heights in the guide (level i starts at Z = 2 + 8 x i mm). - Pressure advance tower: print the outer walls fast (80 to 120mm/s) with no dynamic slowdowns, and ramp the value with height. - Flow cube: needs a single 0.45mm wall line, or spiral vase mode. - First-layer test: pick the 220 or 256 version for your bed and keep it centred. - Resin: print straight on the build plate with no supports. 0.05mm layers, your resin's normal exposure, 4 to 6 bottom layers. Wash and cure before measuring.
Files
- GUIDE.mdmd30 KB
- GUIDE.pdfpdf71 KB
- SP_Calibration_Set_FDM.zipzip1.3 MB
- SP_Calibration_Set_Full.zipzip1.9 MB
- SP_Calibration_Set_Resin.zipzip725 KB
- sp_calcube_20.3mf3mf5.3 KB
- sp_calcube_20.stlstl24 KB
- sp_calcube_40_hollow.3mf3mf5.9 KB
- sp_calcube_40_hollow.stlstl27 KB
- sp_fdm01_overhang_fan.3mf3mf29 KB
- sp_fdm01_overhang_fan.stlstl149 KB
- sp_fdm02_bridge_test.3mf3mf41 KB
- sp_fdm02_bridge_test.stlstl225 KB
- sp_fdm03a_stringing_twin.3mf3mf76 KB
- sp_fdm03a_stringing_twin.stlstl382 KB
- sp_fdm03b_stringing_5pillar.3mf3mf107 KB
- sp_fdm03b_stringing_5pillar.stlstl553 KB
- sp_fdm04_temp_tower_abs_asa.3mf3mf29 KB
- sp_fdm04_temp_tower_abs_asa.stlstl159 KB
- sp_fdm04_temp_tower_petg.3mf3mf25 KB
- sp_fdm04_temp_tower_petg.stlstl136 KB
- sp_fdm04_temp_tower_pla.3mf3mf23 KB
- sp_fdm04_temp_tower_pla.stlstl125 KB
- sp_fdm05a_tol_pegplate.3mf3mf53 KB
- sp_fdm05a_tol_pegplate.stlstl263 KB
- sp_fdm05b_tol_peg.3mf3mf30 KB
- sp_fdm05b_tol_peg.stlstl152 KB
- sp_fdm05c_tol_fitcard.3mf3mf31 KB
- sp_fdm05c_tol_fitcard.stlstl174 KB
- sp_fdm05d_tol_key.3mf3mf2.3 KB
- sp_fdm05d_tol_key.stlstl8.0 KB
- sp_fdm06_first_layer_220.3mf3mf7.0 KB
- sp_fdm06_first_layer_220.stlstl39 KB
- sp_fdm06_first_layer_256.3mf3mf7.0 KB
- sp_fdm06_first_layer_256.stlstl39 KB
- sp_fdm07_flow_singlewall.3mf3mf6.9 KB
- sp_fdm07_flow_singlewall.stlstl35 KB
- sp_fdm08_pa_tower.3mf3mf14 KB
- sp_fdm08_pa_tower.stlstl75 KB
- sp_fdm09_small_features.3mf3mf51 KB
- sp_fdm09_small_features.stlstl282 KB
- sp_fdm10_roundness_belt.3mf3mf31 KB
- sp_fdm10_roundness_belt.stlstl145 KB
- sp_resin11_exposure_matrix.3mf3mf71 KB
- sp_resin11_exposure_matrix.stlstl379 KB
- sp_resin12_min_features.3mf3mf105 KB
- sp_resin12_min_features.stlstl515 KB
- sp_resin13a_hollow_drain.3mf3mf30 KB
- sp_resin13a_hollow_drain.stlstl130 KB
- sp_resin13b_drain_plugs.3mf3mf95 KB
- sp_resin13b_drain_plugs.stlstl471 KB